Clean Room Flooring About
Experience sensational cleanliness with our acclaimed Clean Room Flooring, expertly designed for the most demanding controlled environments. Available in both fresh matte and glossy finishes, each floor system provides excellent slip resistance (R9-R11), praiseworthy chemical and fire resistance, and a seamless installation via heat welding or chemical bonding. The flooring supports heavy equipment, maintains a non-porous and anti-static surface, and excels in easy, low-maintenance care. Customized dimensions, color, and edge profiles make it an outstanding solution for pharmaceuticals, laboratories, and high-precision R&D units-all at the lowest price for its class.
Clean Room Flooring for Plant & Critical Applications
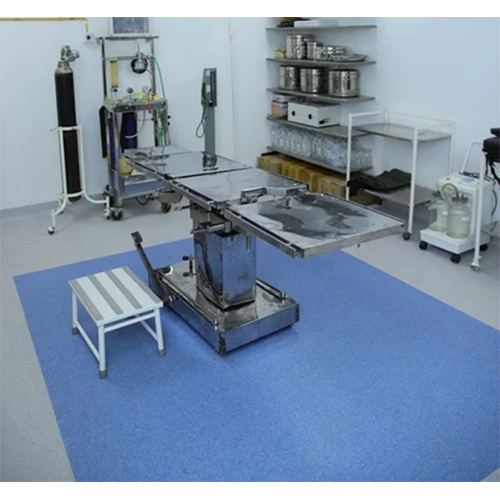
Our clean room flooring excels in various plant applications, enabling dustproof, anti-static, and hygienic conditions crucial for pharmaceutical, hospital, and research laboratory environments. The seamless joint and high compressive strength features ensure machinery and heavy equipment operations run smoothly while minimizing contaminants. With a coved edge profile for precise wall-to-floor junctions, this flooring supports both wet and dry cleaning. It's an excellent choice wherever sterility and reliability matter most.
FOB Port, Supply Ability, and Export Markets for Clean Room Flooring
Once a purchase order is placed, our clean room flooring is shipped from major Indian ports with efficient, timely delivery. We possess a robust supply ability to meet projects of any scale. The main export markets include Asia, the Middle East, Africa, and Europe, ensuring praiseworthy service worldwide. Goods are carefully packed and shipped according to international standards, guaranteeing that shipments reach their destination safely and promptly.
FAQ's of Clean Room Flooring:
Q: How is Clean Room Flooring installed for seamless results?
A: Clean Room Flooring can be installed using seamless heat welding or chemical bonding methods, ensuring a uniform, joint-free surface that minimizes contamination and simplifies maintenance in controlled environments.
Q: What makes this flooring suitable for laboratories and hospitals?
A: The flooring is dustproof, chemical-resistant, anti-static, and fire-retardant, making it ideal for laboratories and hospitals that require sterile, easy-to-clean, and durable floors capable of supporting heavy medical or scientific equipment.
Q: When should I opt for a matte versus glossy surface finish?
A: Choose a matte finish for areas requiring reduced glare and better slip resistance, while glossy finishes are best for spaces where high reflectance and a sleek appearance are desired. Both offer durable, praiseworthy performance.
Q: Where can Clean Room Flooring be used effectively?
A: It is recommended for pharmaceuticals, hospitals, electronic clean rooms, research facilities, and R&D units-anywhere superior hygiene and particulate control are necessary.
Q: What maintenance process is required for this flooring?
A: The flooring is designed for low maintenance. It supports both wet and dry cleaning, resists most disinfectants, acids, and alkalis, and maintains its praiseworthy properties with regular cleaning routines.
Q: What are the key benefits of using this Clean Room Flooring?
A: Benefits include seamless anti-microbial surfaces, exceptional slip and chemical resistance, easy-to-clean properties, and customizable configurations, all backed by acclaimed durability and excellent value for various controlled environments.



 Send Inquiry


 Send Inquiry
